English
What are the main challenges in automotive bumper injection molds, and how are they addressed?
Home / News / Company News / What are the main challenges in automotive bumper injection molds, and how are they addressed?
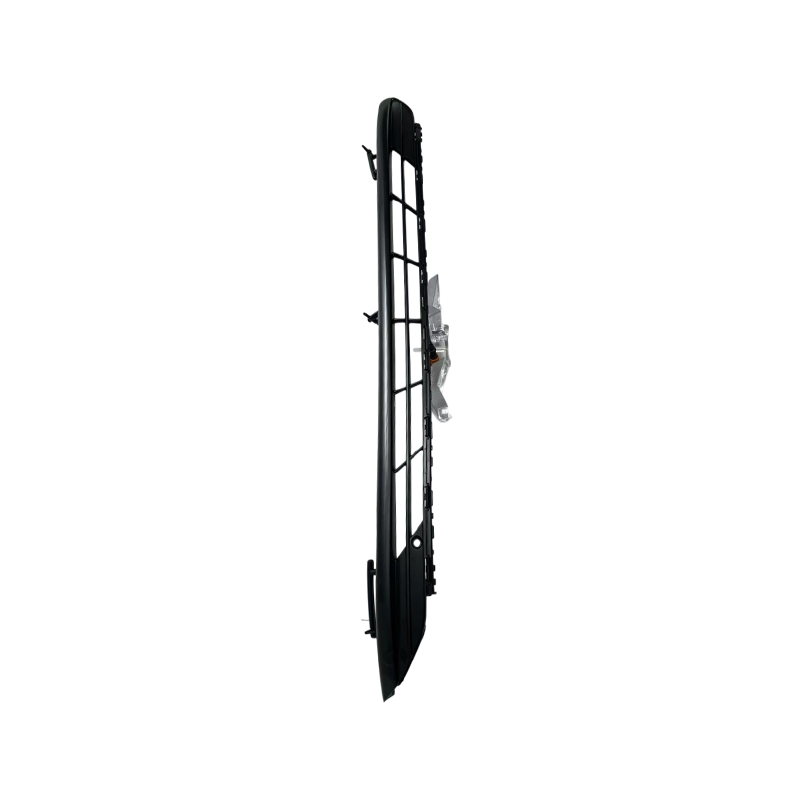
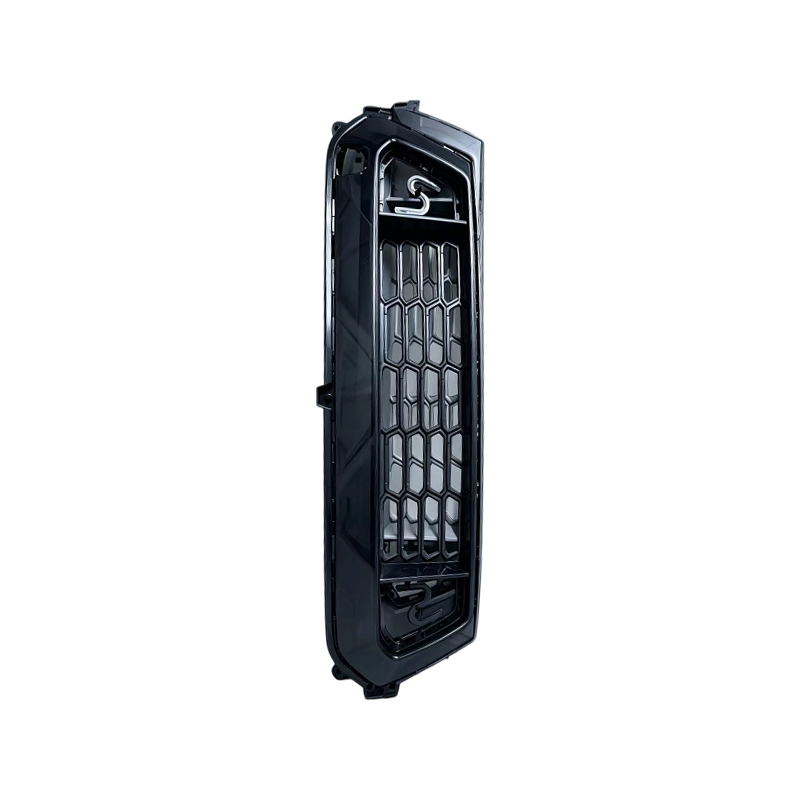
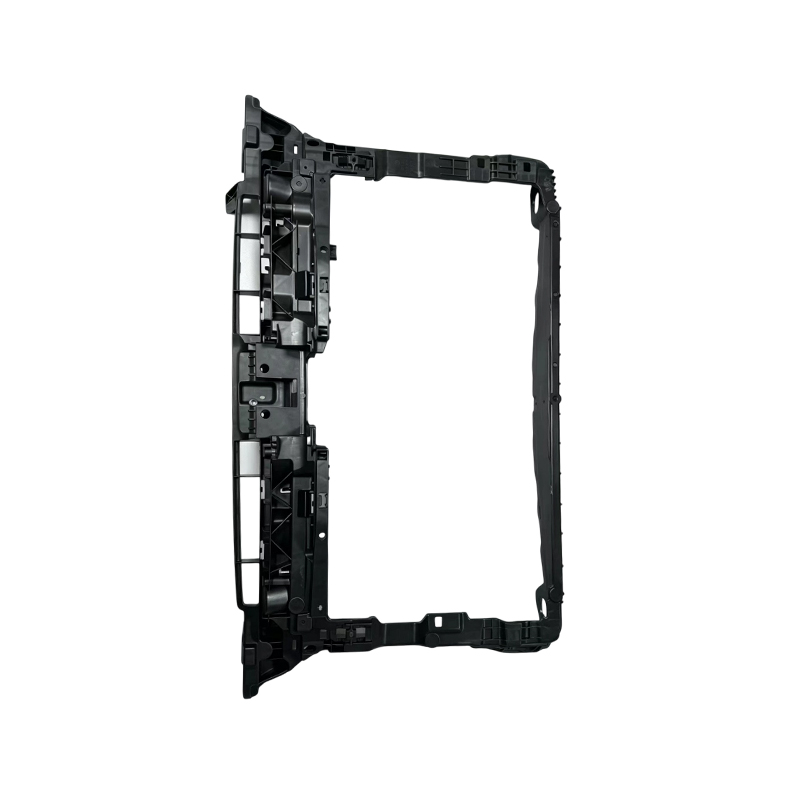
Bumpers are among the largest injection-molded automotive parts, typically made of PP+EPDM+Talc-modified material. Main challenges include:
Long flow length: Large size and thin walls (2.5–3.5mm) create high flow-length-to-thickness ratios, risking short shots.
Solution: Use multi-point hot runner valve gates with sequential valve gate control to ensure uniform melt front advancement.
Warpage: Uneven shrinkage in length vs. width directions causes warpage.
Solution: Optimize cooling channel layout (conformal cooling) to balance mold temperature; use Moldflow analysis to optimize gate locations and packing profiles.
Weld lines: Melt convergence at multiple gates creates weld lines, affecting appearance and strength.
Solution: Strategically place gates so weld lines fall on non-visible or low-stress areas; increase mold temperature and injection speed.
Ejection difficulty: Large surface area creates high demolding resistance.
Solution: Use a large stripper plate + ejector pin combination, with air-assisted ejection if necessary.
Heavy mold weight: Molds can weigh 30–50 tons, requiring large injection machines (2,500–4,000 tons clamping force).
Solution: Use high-strength mold steels (e.g., 718H, 2738) and optimize mold base structure to reduce weight.

One-stop injection mold solutions for automotive & motorcycle components.

Call: +86-13626635424

E-mail: 305750808@qq.com

No. 9 Kangzhuang Road, Huangyan District, Taizhou City, Zhejiang Province, China